Heavy Steel Fabrication for Construction and Mining Equipment
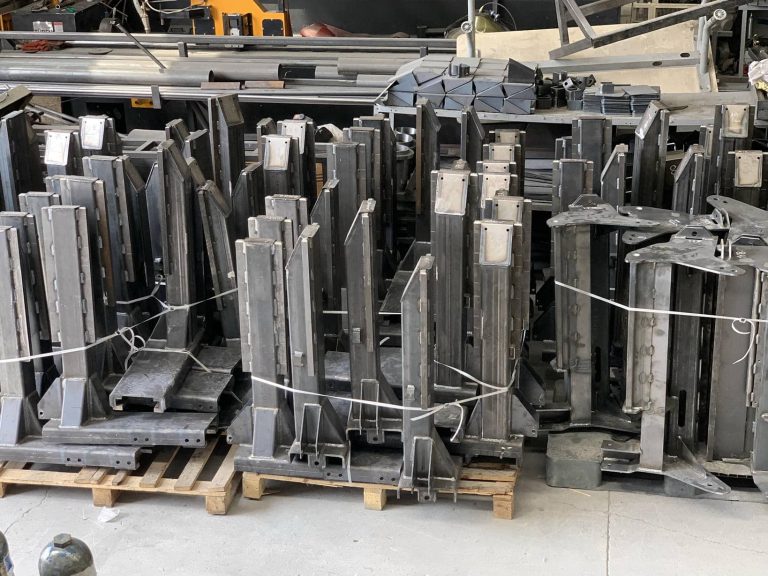
Booms, frames, box beams, buckets, skids, platforms, cylinder parts and wear parts for construction, mining and drilling machinery. Welded to EN 1090 EXC3 and machined after welding in İzmir.
- EN 1090 EXC3Fatigue-loaded welds
- 180 mmPlate cutting
- 12 tCrane capacity
- HardoxWear plate
- Ø4,200 mmMachining
Heavy Weldments That Take Load and Wear
Construction and mining machines work under shock, fatigue and abrasion. Their welded structures need qualified procedures, full-penetration welds where the drawing asks for them, and machining that keeps pin bores aligned. Our EN 1090-2 EXC3 and ISO 3834-2 certification covers exactly that level of work.
We cut plate up to 180 mm, weld high-strength and wear-resistant steels, and machine bores, faces and bolt patterns on boring mills with 4,500 mm travel. Parts up to 12 tonnes are handled with overhead cranes.
Capability
- Plateup to 180 mm, plasma
- SteelsS355–S960, Hardox 400/500
- WeldingEN 1090 EXC3, ISO 3834-2
- NDTVT, PT, MT, UT
- Machining4,500 mm travel, Ø4,200 mm
- Handling12 t cranes
What We Make for Heavy Equipment
Frames and Box Beams
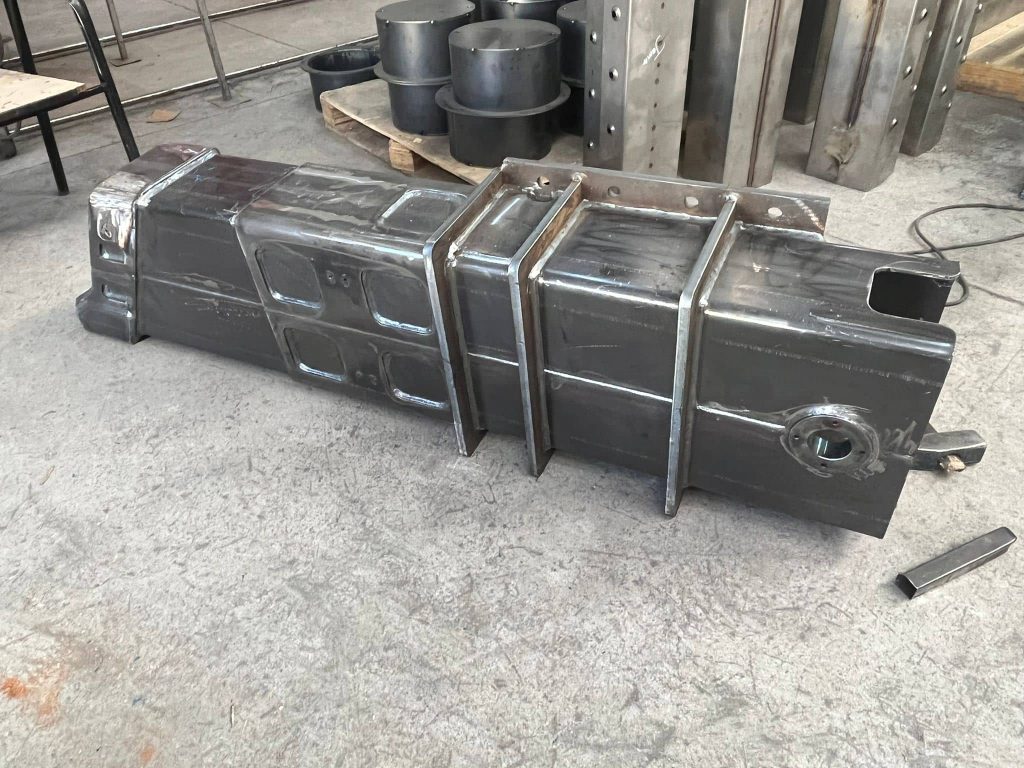
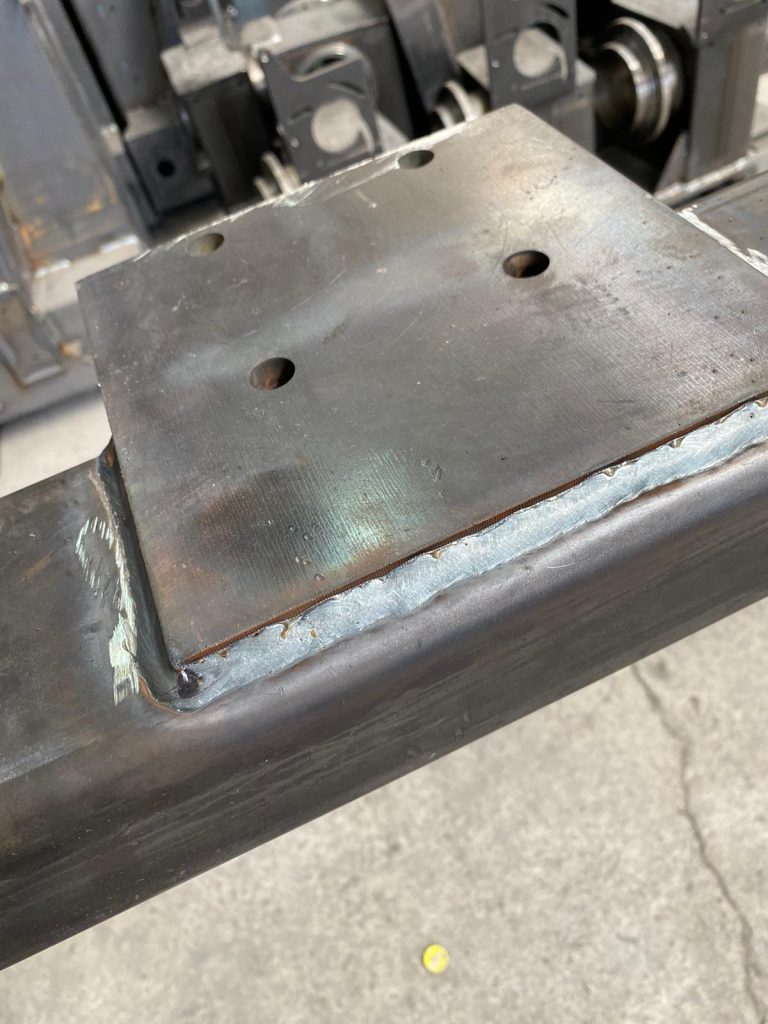
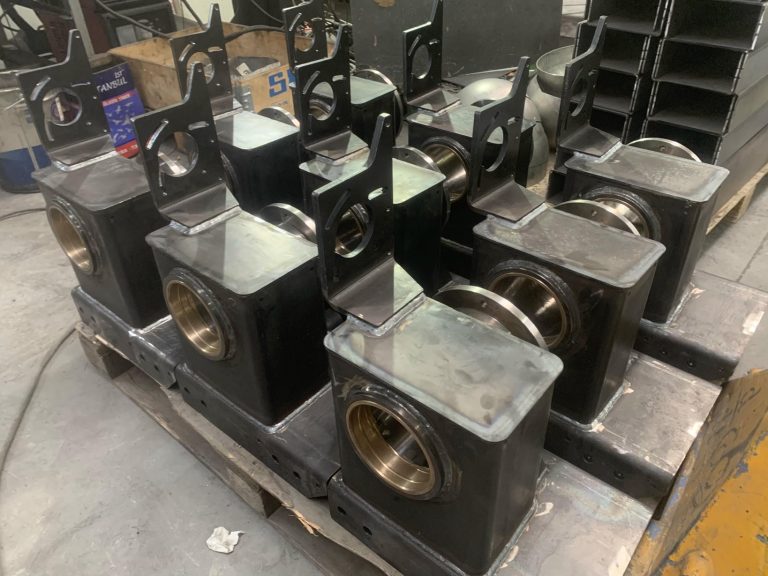
Main frames, sub-frames and box beams with machined pin bores and mounting pads.
Cylinder Barrels and Rods
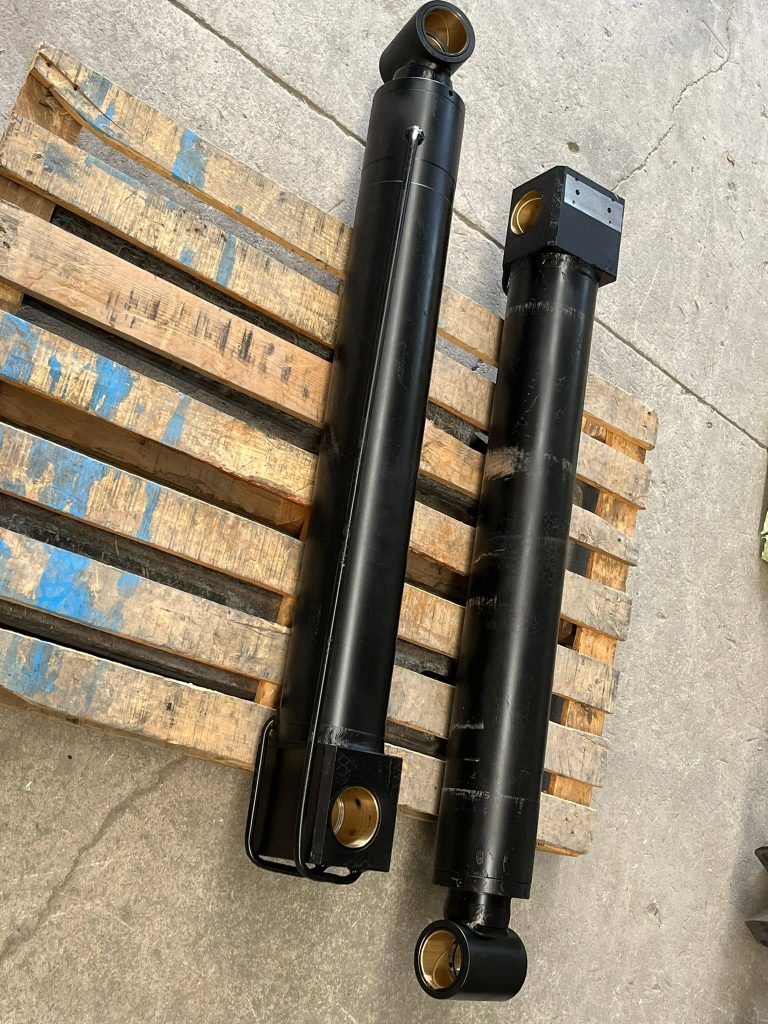
Hydraulic cylinder tubes with welded eyes and clevises, and turned piston rods.
Piston rods →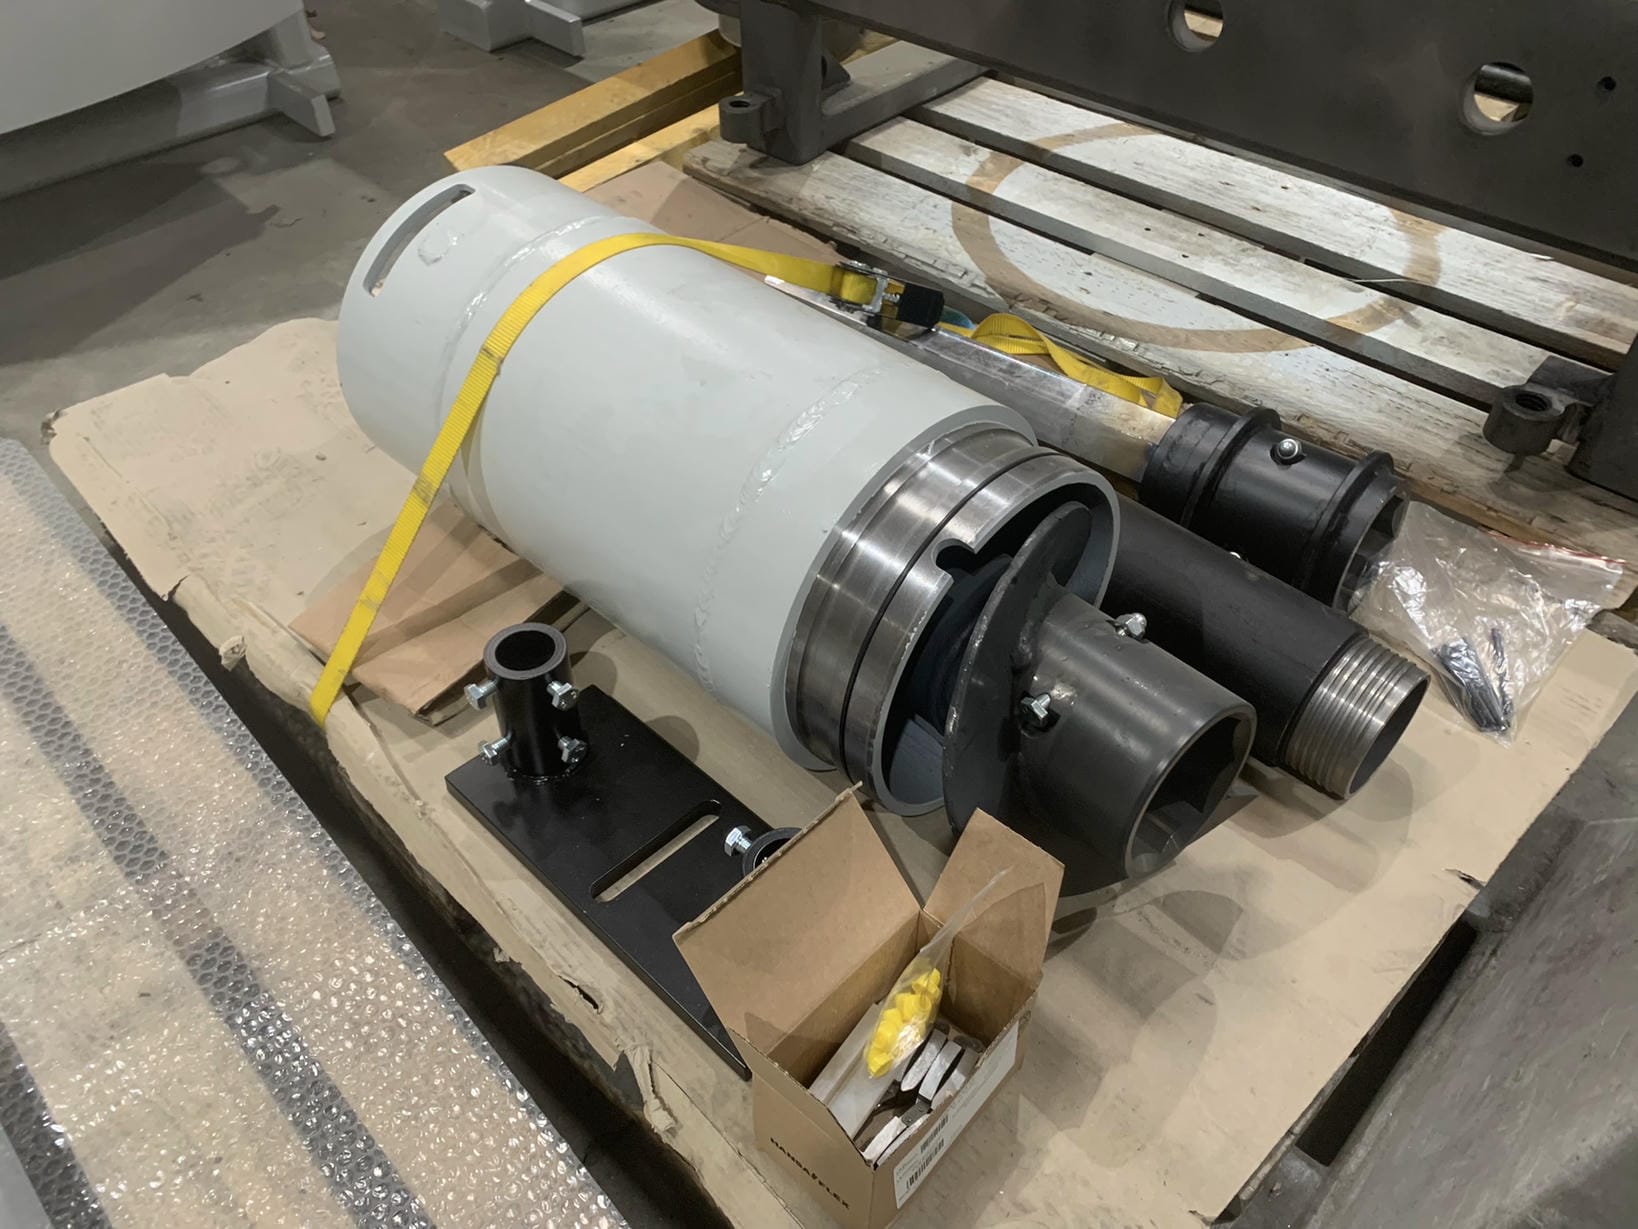
Jacking Pipes and Casings
Rolled and welded pipes with machined joints for trenchless and drilling work.
Jacking pipes →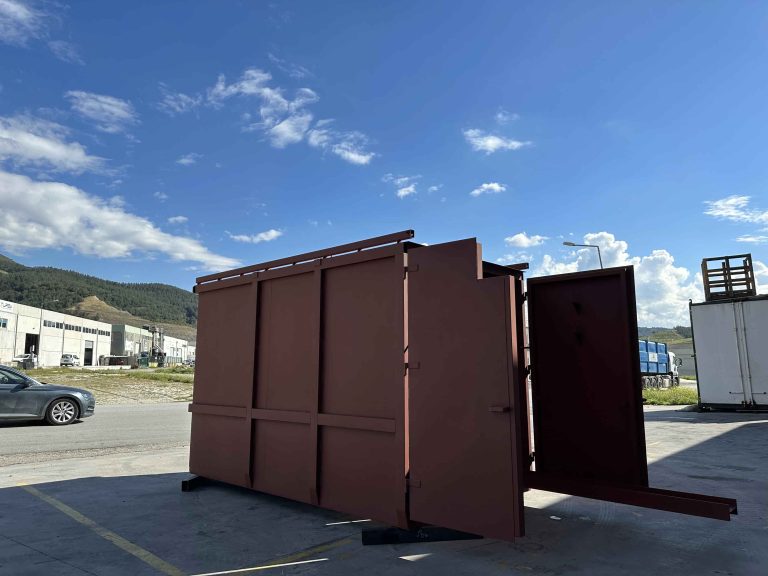
Containers and Skids
Site containers, tool boxes, skids and platforms built to your load case.
Steel containers →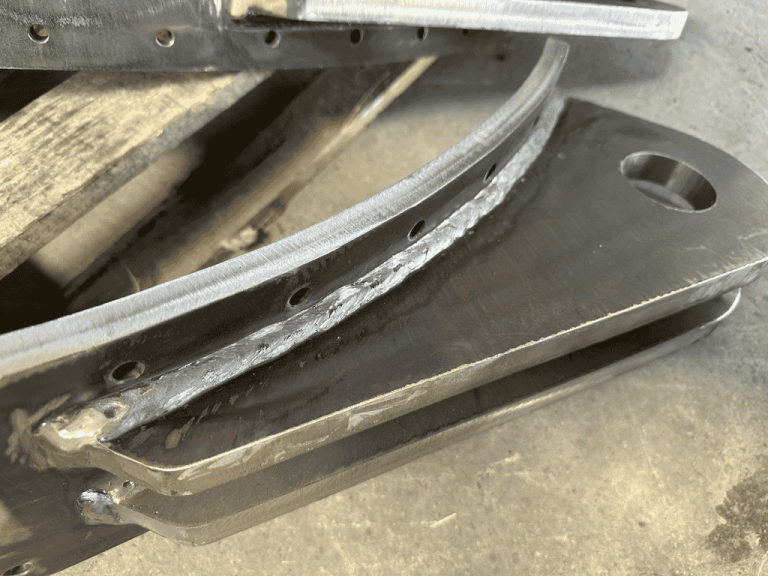
Wear Parts and Liners
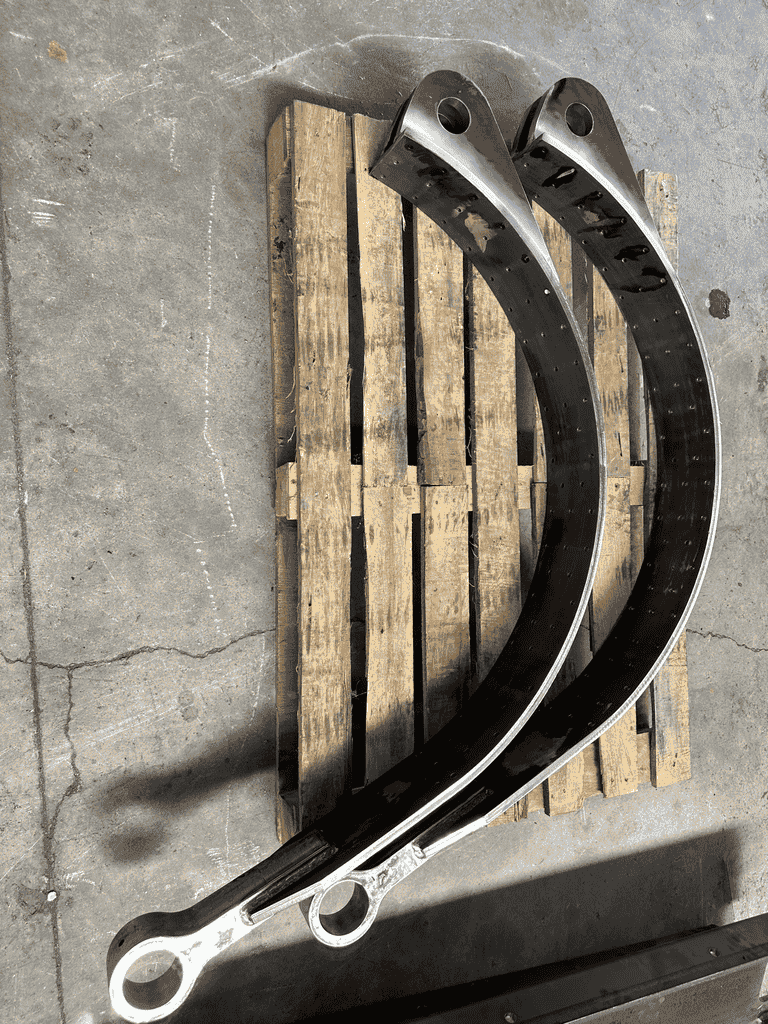
Cutting edges, liners and segments in Hardox, cut and bent to drawing.
Machined Weldments
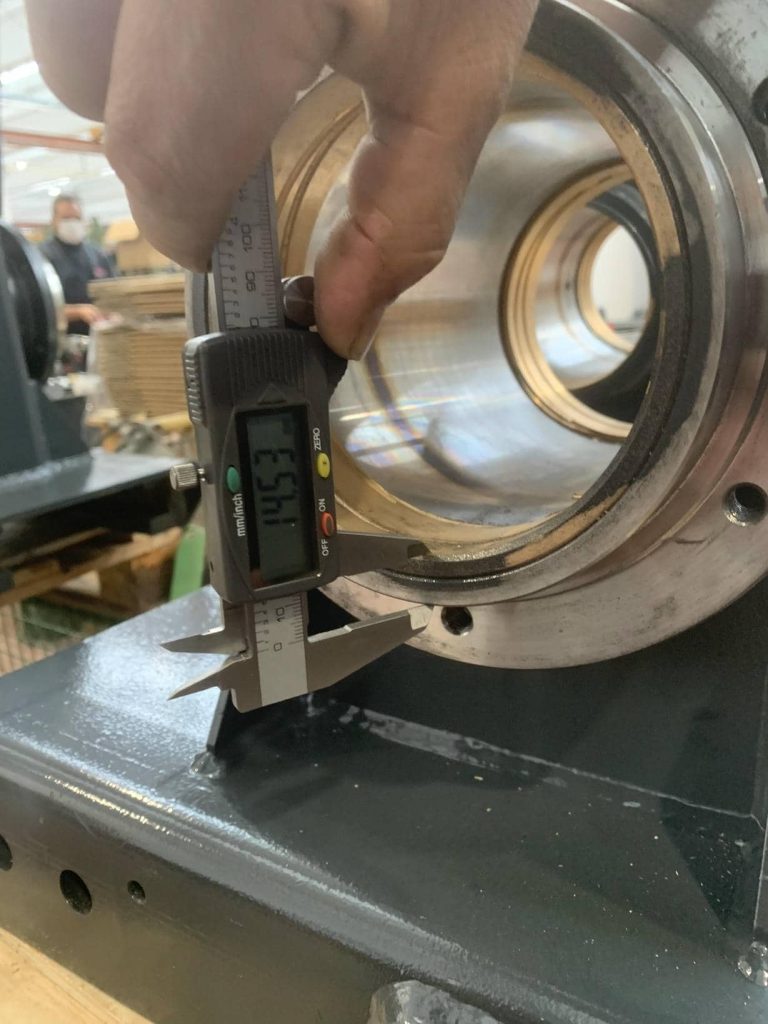
Heavy weldments finish-machined on boring mills so pin bores stay aligned.
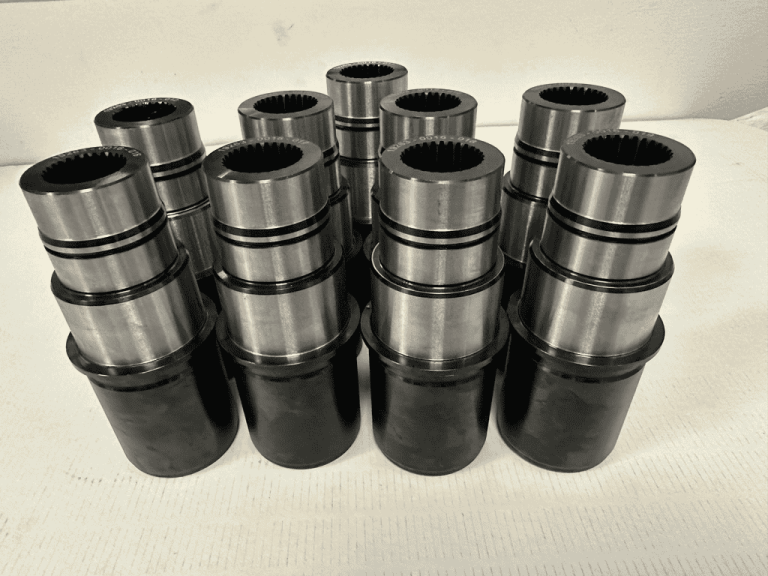
Large-part machining →Heavy Fabrication in Practice
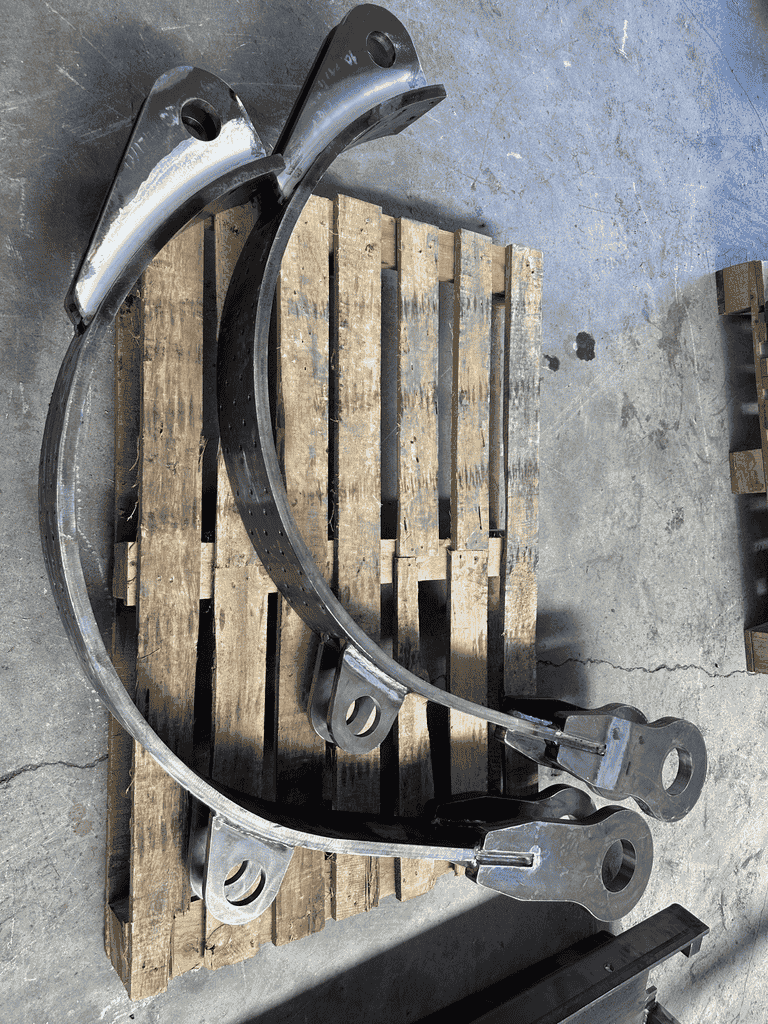
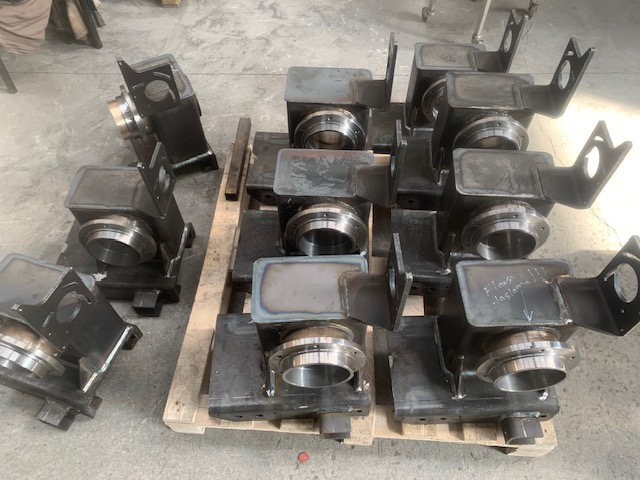
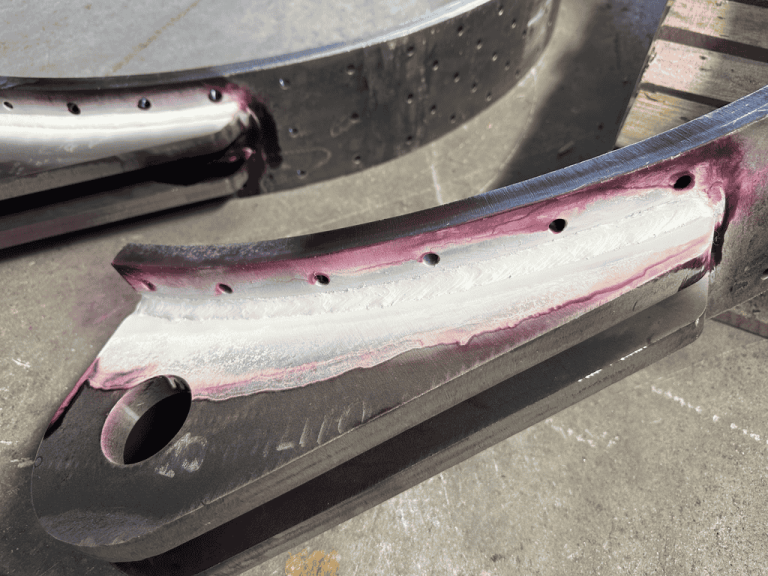
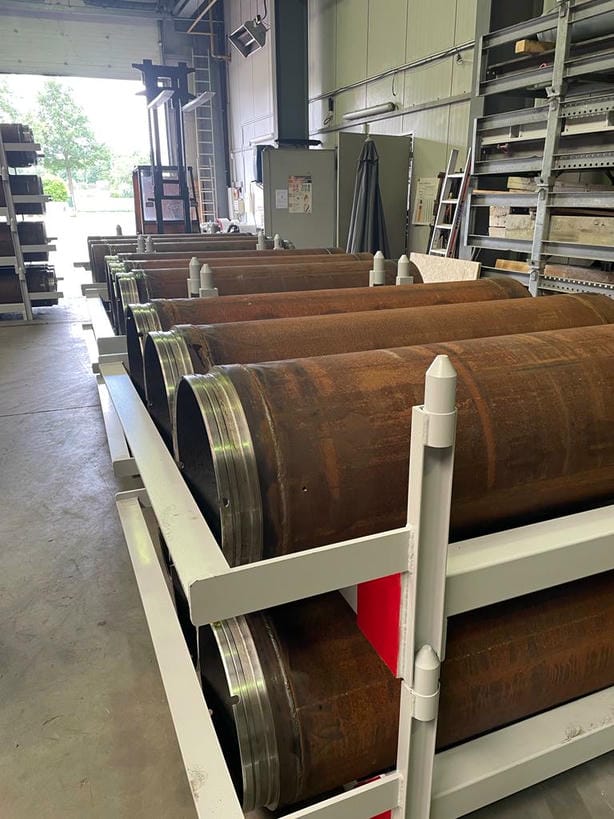
Questions from Construction and Mining Equipment Builders
Can you weld high-strength steel?
Yes. S355 up to S960 and wear plates such as Hardox are welded with qualified procedures, preheat and suitable consumables.
Do you do UT on welds?
Yes. Ultrasonic, magnetic particle and penetrant testing are carried out when the drawing or ITP requires them.
How heavy can parts be?
Our overhead cranes handle parts up to 12 tonnes.
Can you machine pin bores after welding?
Yes. Bores and faces are line-bored and milled on boring mills with 4,500 mm travel.
Are you certified for structural work?
Yes. EN 1090-1 FPC and EN 1090-2 up to EXC3, ISO 3834-2 and ISO 9001.
Construction and Mining Equipment Fabrication in Türkiye
Heavy equipment builders in Europe face long lead times for large weldments. We add capacity for frames, booms, box beams and wear parts, with certified welding and heavy machining at one supplier.
Certified welding for load and fatigue
EXC3 under EN 1090-2 covers fatigue-loaded structures. Our welders are qualified to EN ISO 9606-1, procedures to ISO 15614, and NDT is done to your plan. See welding and fabrication.
Machined after welding
See large-part machining and the machine park, or send your drawing.
Send drawings for heavy weldments.
Include material, weld class, NDT and weights. We reply with feasibility, lead time and price.