Large-Part Machining in Türkiye up to Ø4,200 mm and 12 Tonnes
Heavy flanges, rings, drums, housings and welded machine beds, turned, bored and milled to your drawing. Our family group’s 1,600 m² machining plant in Kemalpaşa handles parts that standard machining centres cannot hold, with 12-tonne crane capacity and machining after welding on the same order.
- Ø4,200 mmVertical turning
- 4,500 mmBoring & milling travel
- 6,000 mmTurning length
- 12 tCrane capacity
- 1,600 m²Machining plant
Where this work is done
Large-part machining and large welded parts are done at our family group’s heavy-machining plant in Kemalpaşa, İzmir. Nika Steelworks quotes the order, manages it, inspects the parts and stays your single contact.
When the Part Is Too Big for a Standard Machine Shop
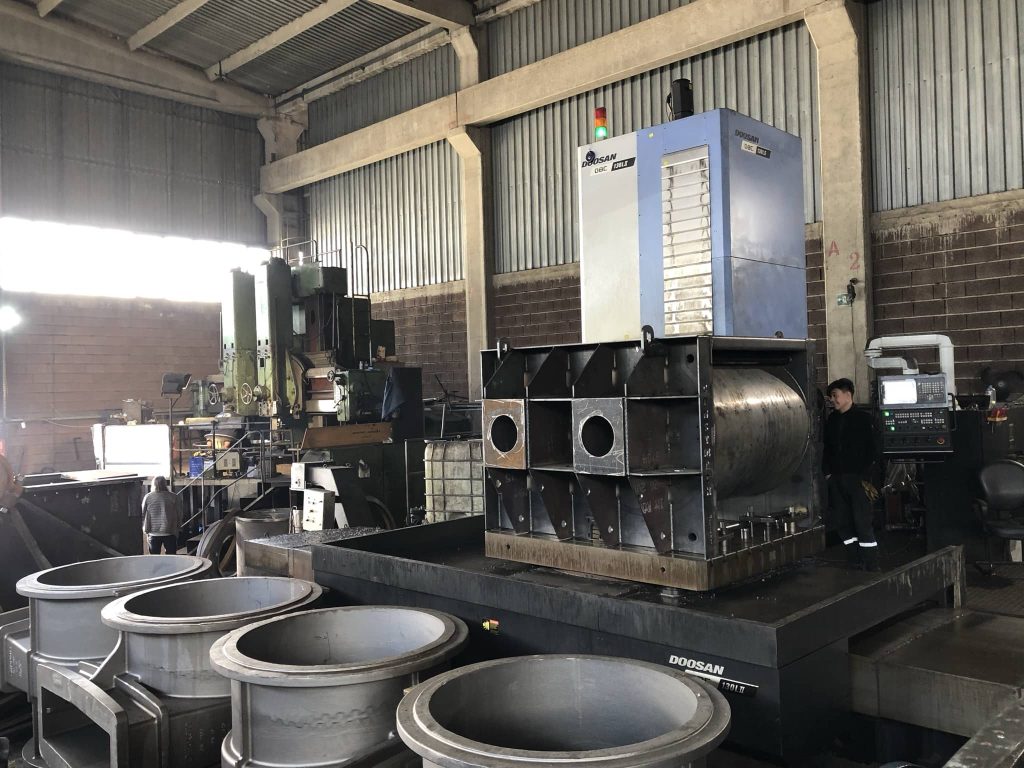
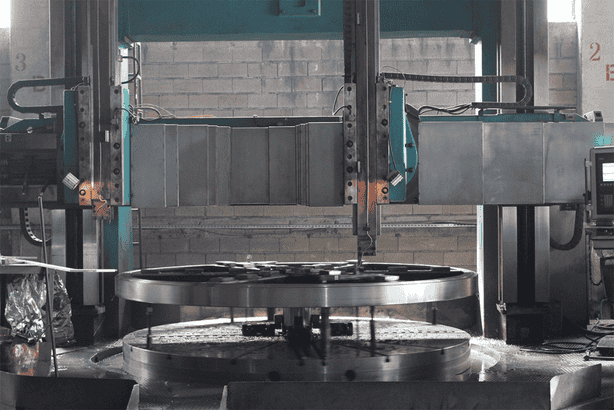
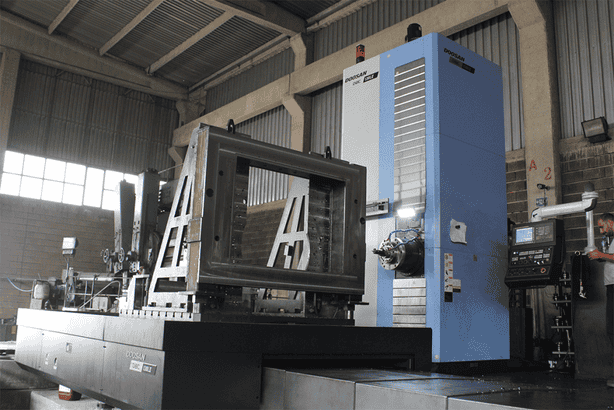
Most machine shops stop at a one-metre table. We start where they stop. Vertical lathes turn parts up to Ø4,200 mm and 2,500 mm high. Doosan, Scharmann and WFL boring mills reach 4,500 × 2,500 × 2,000 mm of travel. Long-bed lathes turn shafts and rollers up to 6,000 mm. Overhead cranes lift parts up to 12 tonnes.
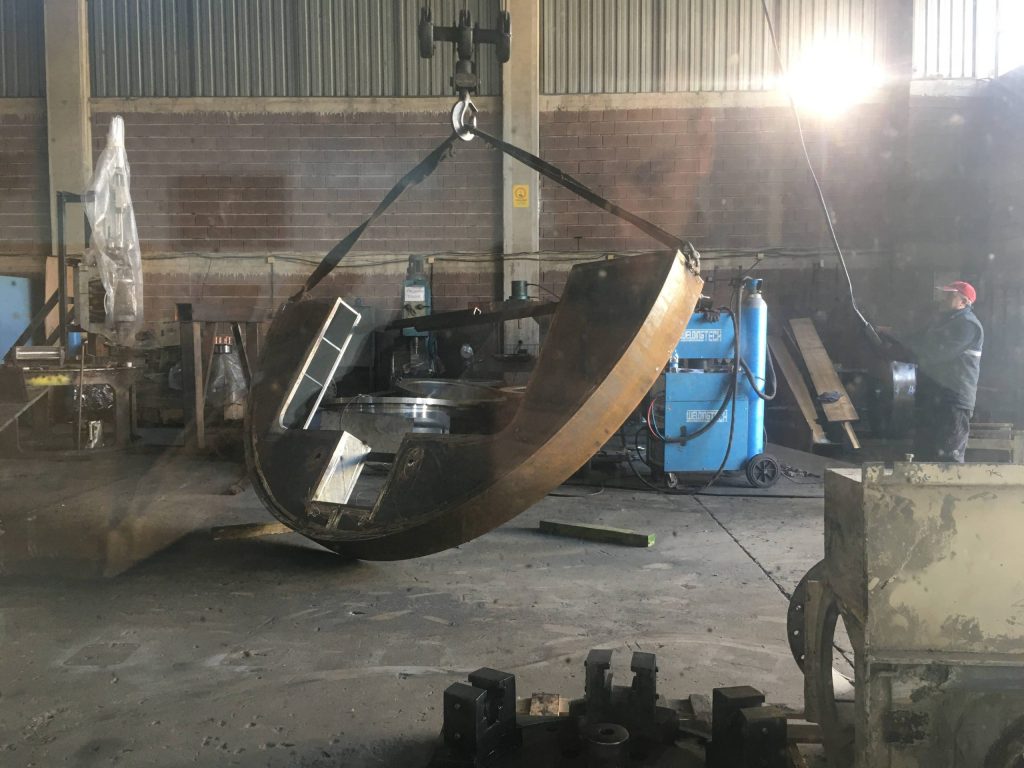
Large parts rarely come as a solid block. They are rolled rings, welded drums, fabricated housings and machine beds. They are welded and finish-machined at the Kemalpaşa plant, so the datum stays in one place from fit-up to final measurement. Nika Steelworks inspects and documents every order.
Large-part capacity
- Vertical turningØ4,200 × 2,500 mm
- Boring & milling4,500 × 2,500 × 2,000 mm
- Largest table2,000 × 1,500 mm
- Long turningØ2,400 × 6,000 mm
- Crane capacity12 tonnes
- ControlsFanuc · Siemens
- MeasuringCMM measurement
Large-Part Machines
The full list with every machine is on the machine park page.
Which machine for which part
| Part | Machine | Maximum size |
|---|---|---|
| Flanges, rings, slewing-ring seats | Dalian YiMei CKQ5240, CK 123, Schiess CU 1250 | Ø4,200 × 2,500 mm |
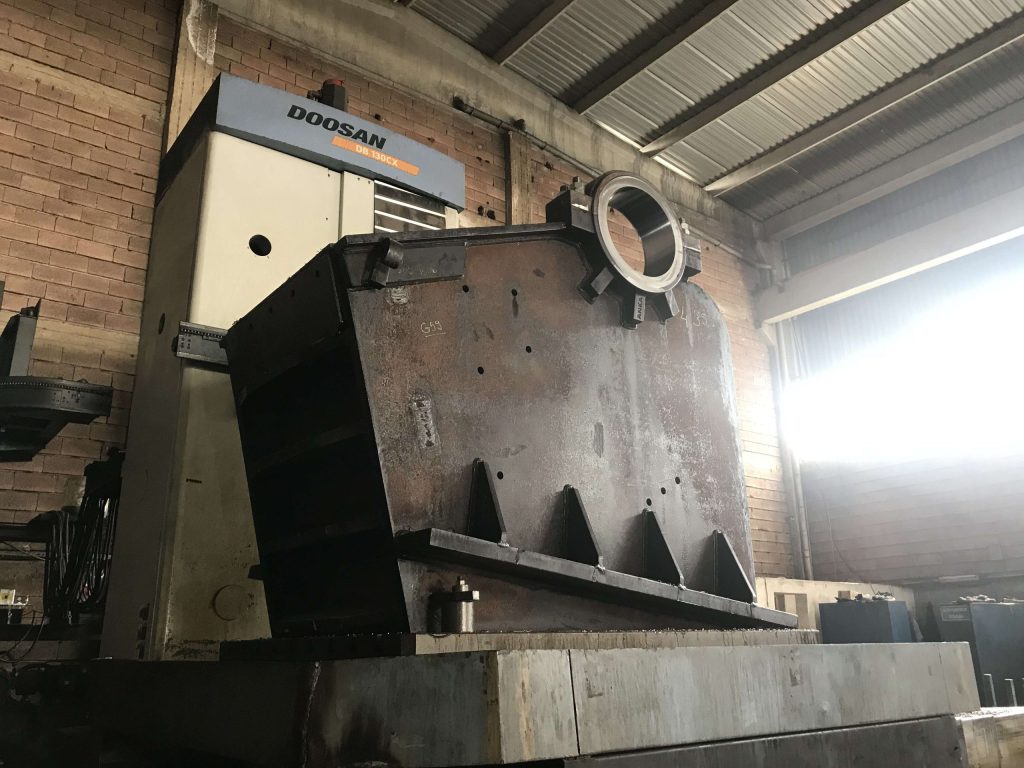
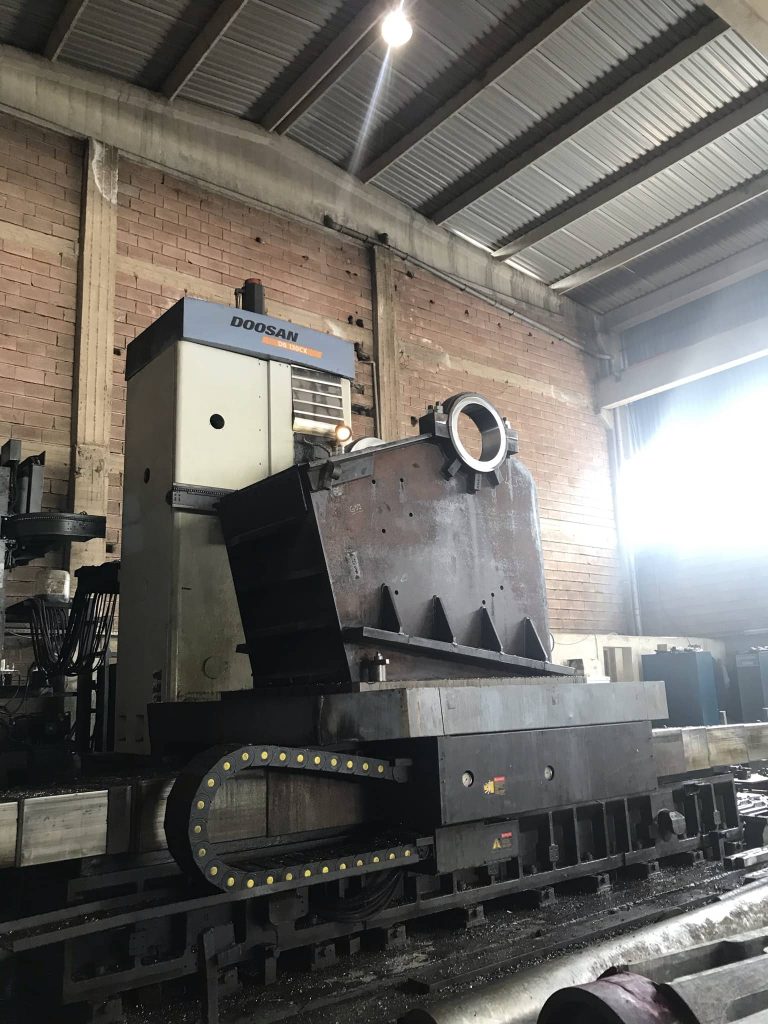
| Machine beds, bases, frames | Doosan DBC 130L II / CX | 4,500 × 2,500 × 2,000 mm |
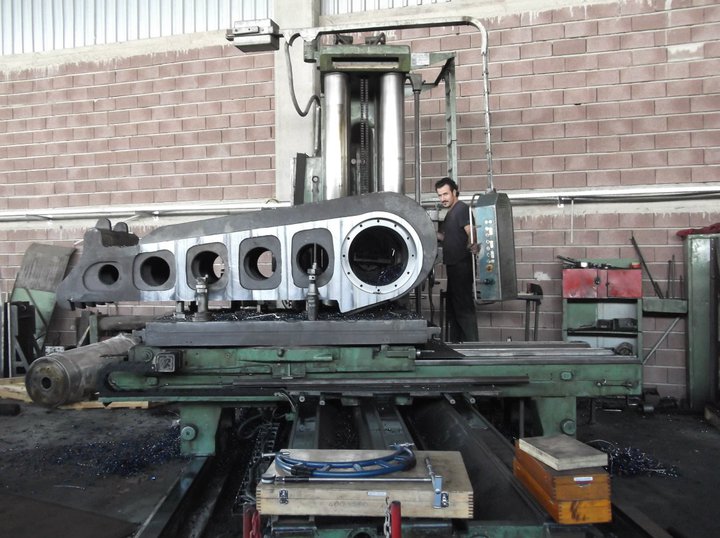
| Gear and bearing housings | Scharmann FWH, WFL BF125 | 2,800 × 2,000 × 2,000 mm |
| Shafts, rollers, drums | Manual lathe, ZMM Sliven CU 1250 | Ø2,400 × 6,000 mm |
| Heavy parts up to | Overhead cranes | 12 tonnes |
What We Machine
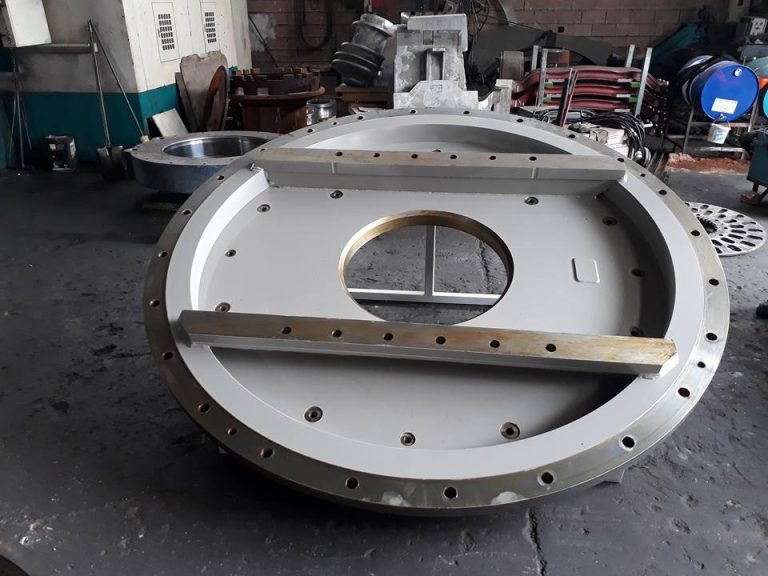
Flanges and Rings
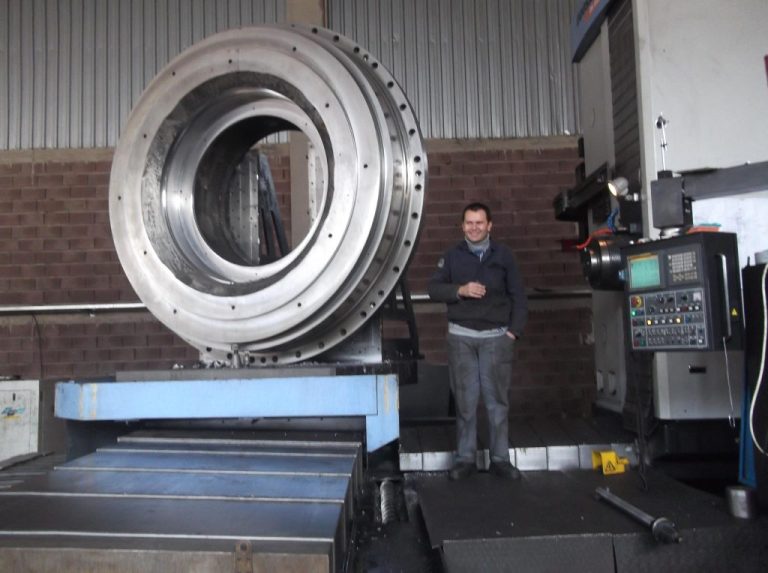
Large flanges, bearing rings and slewing-ring seats turned flat and true on vertical lathes.
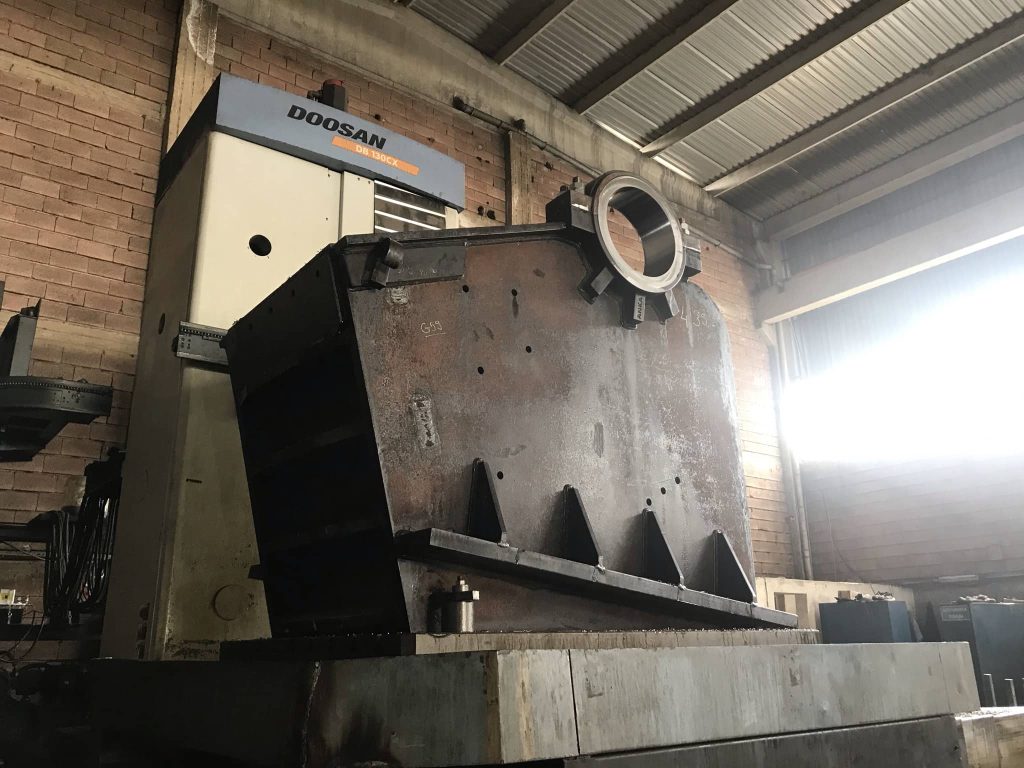
Machine Beds and Bases
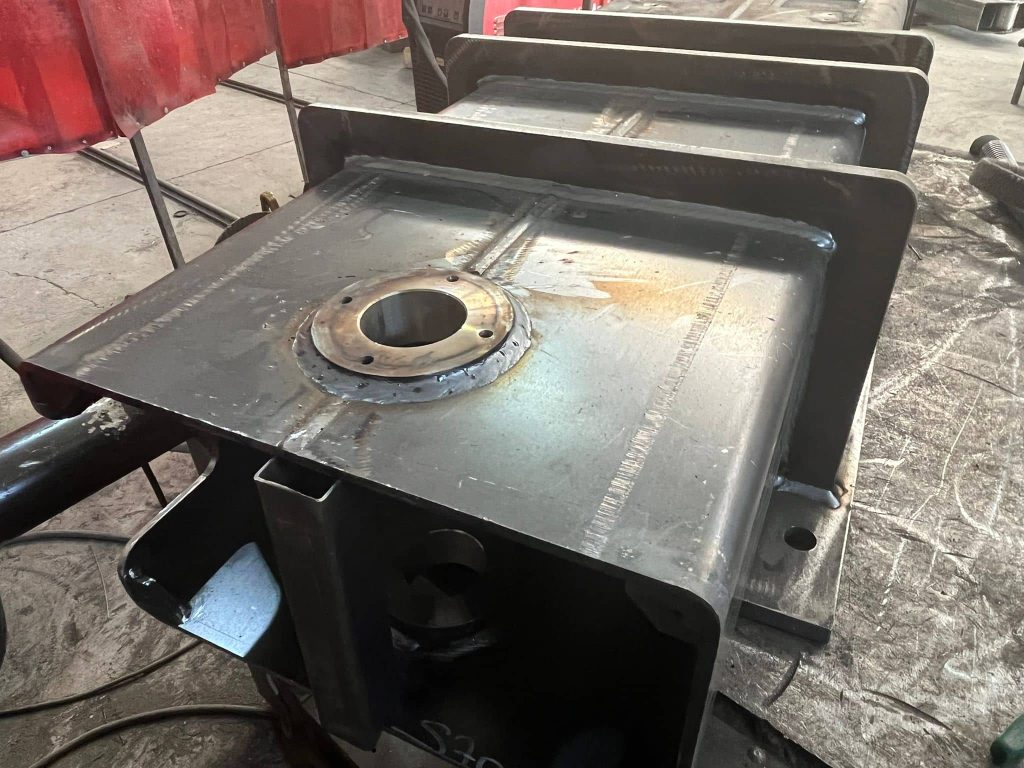
Welded beds and bases milled on datum faces and bored for gearboxes, motors and guides.
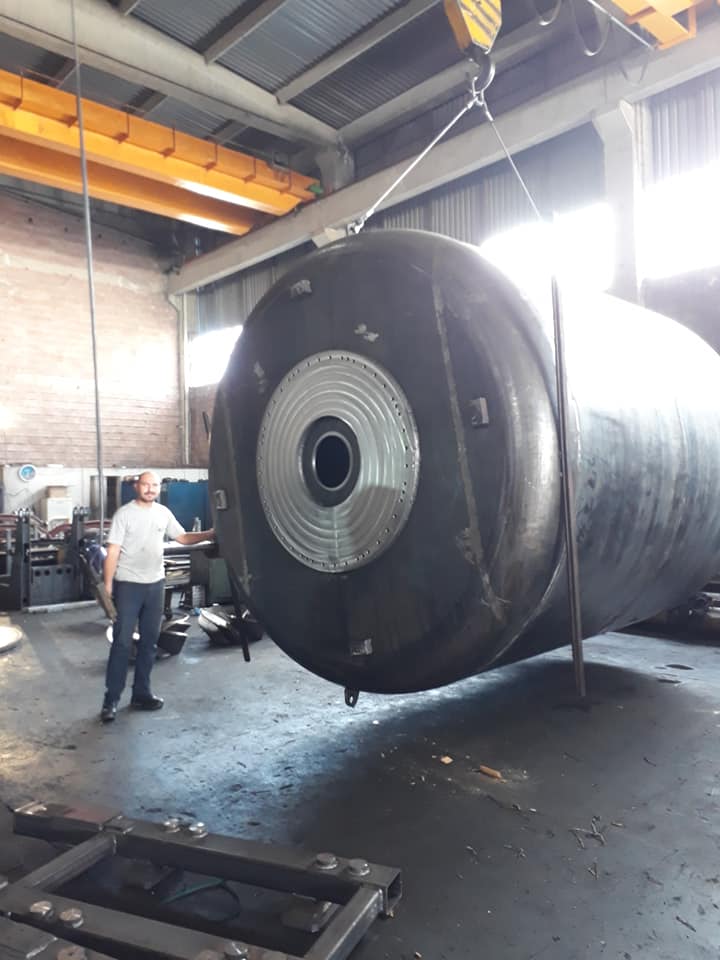
Drums and Shells
Rolled and welded drums with turned diameters, machined flanges and bearing seats.
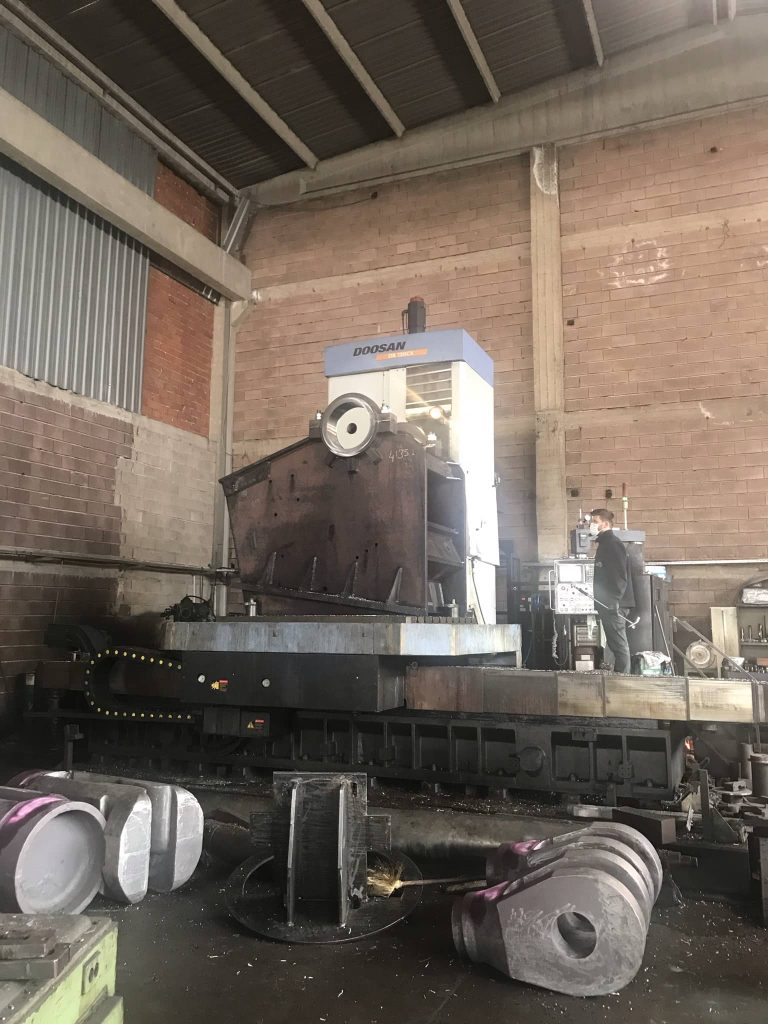
Housings
Gear, bearing and valve housings bored and milled on several faces in few set-ups.
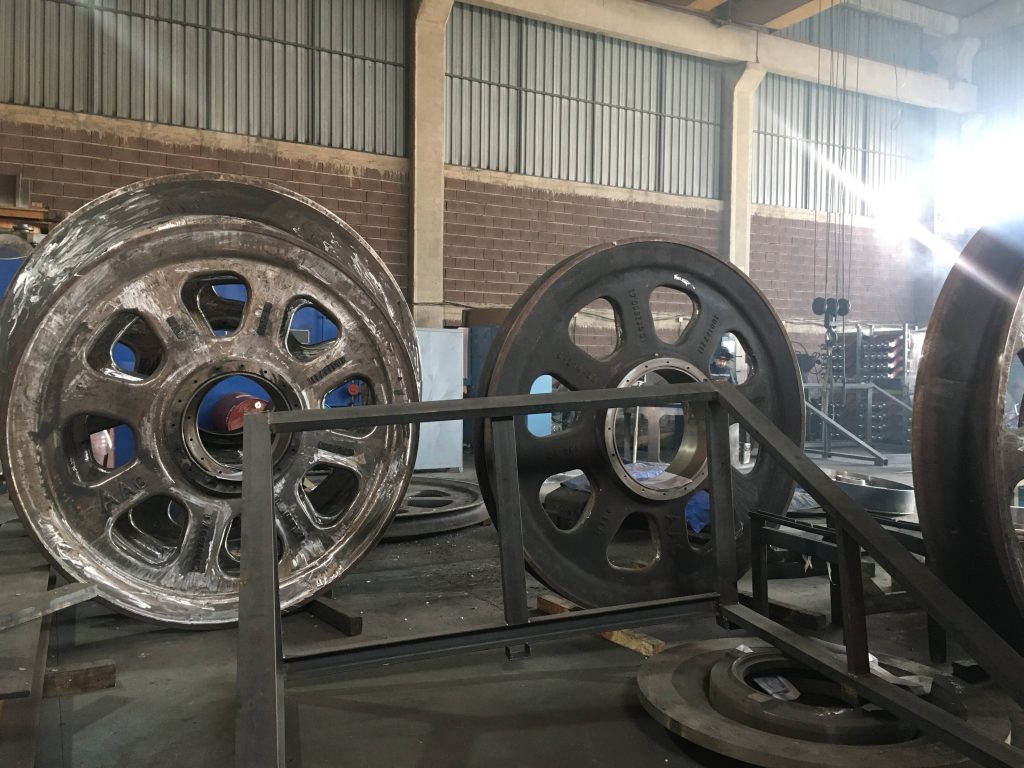
Wheels and Sheaves
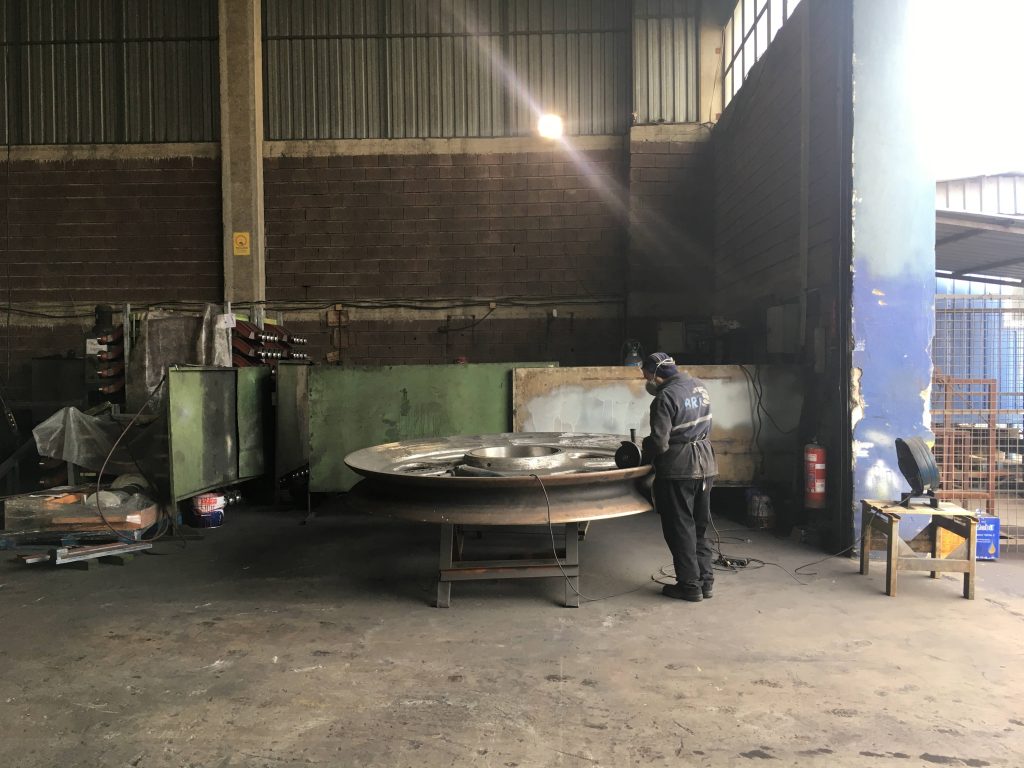
Spoked wheels and rope sheaves turned on hub, rim and groove after welding.
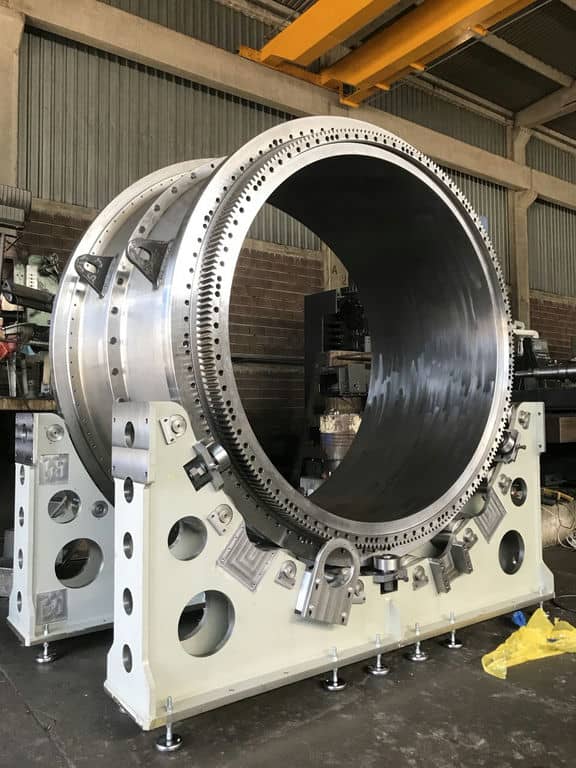
Assemblies
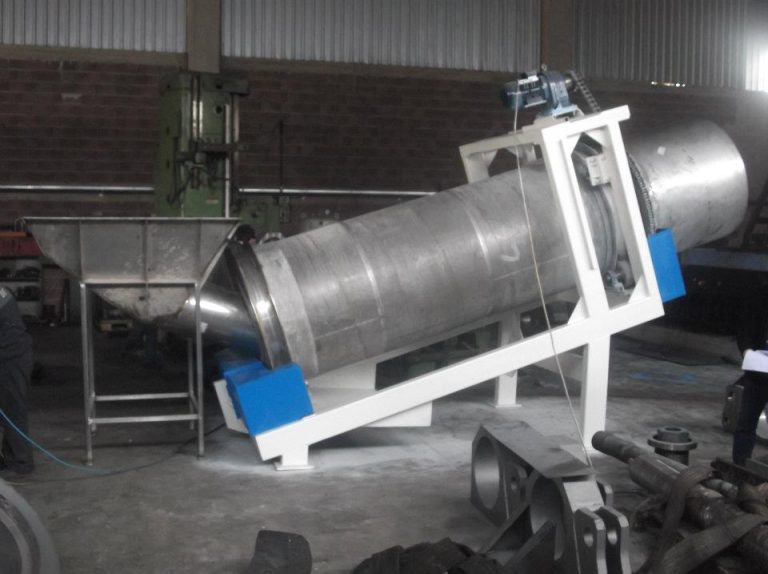
Machined parts fitted into complete assemblies, such as our large rotary mandrel.
See the project →Large Welded Parts, Machined After Welding
Datums agreed first
Datum faces, machining stock and critical bores are agreed during the drawing review.
Welded with stock
The part is cut, rolled and welded with extra material where it will be machined.
Checked for distortion
Large weldments are measured before machining, and stress-relieved when the drawing asks for it.
Machined in few set-ups
Faces, bores and bolt circles are machined on one machine where possible, to keep their relation.
Measured
Critical dimensions are measured by CMM and recorded.
Protected and shipped
Machined faces are protected, the part is coated, cradled and shipped by road or container.
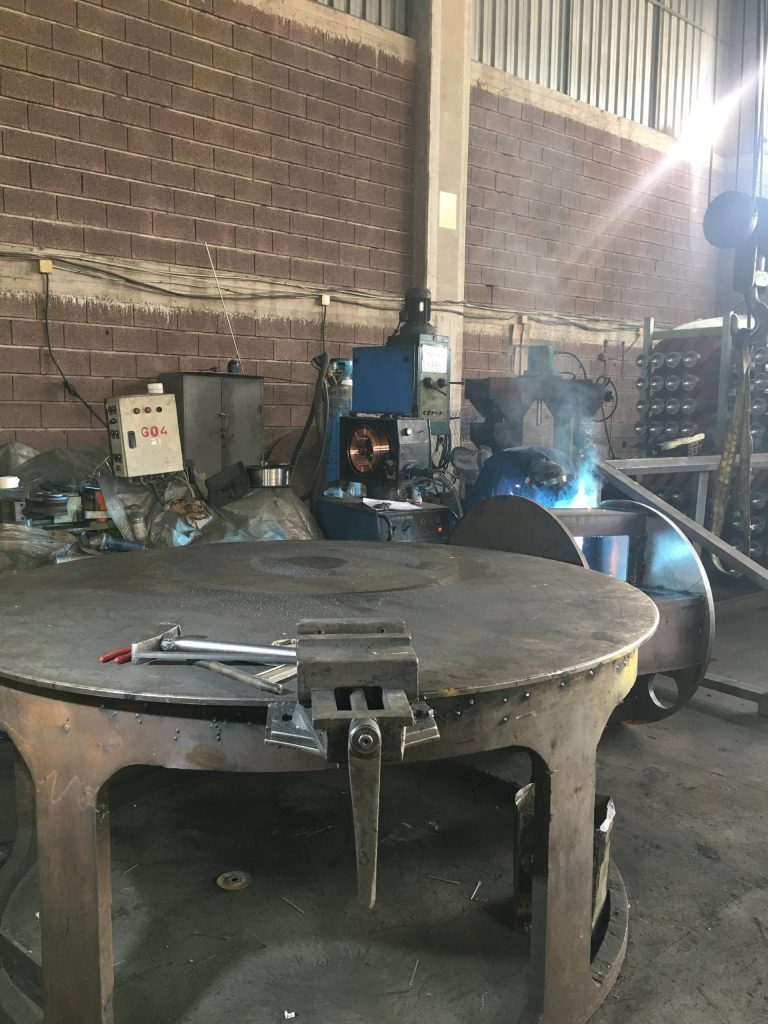
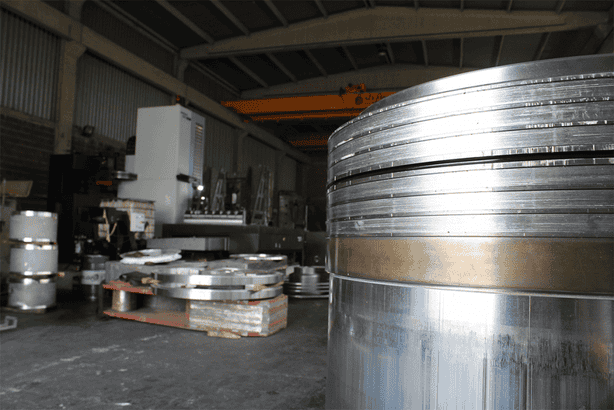
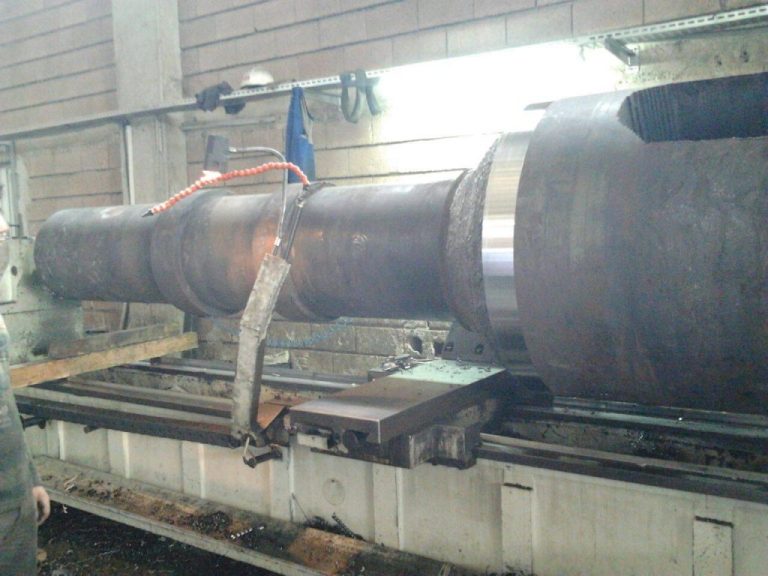
Large-Part Machining in Practice
Questions About Large-Part Machining
What is the largest part you can machine?
Vertical turning up to Ø4,200 mm and 2,500 mm high, boring and milling travel up to 4,500 × 2,500 × 2,000 mm, and turning up to 6,000 mm long.
How heavy can a part be?
Our cranes lift up to 12 tonnes. For heavier or awkward parts, send the drawing with the weight and we confirm handling and the machine.
Can you weld the part and machine it too?
Yes. Large weldments are welded and machined at the Kemalpaşa plant, with machining stock planned at fit-up. Smaller welded parts and series are made at Nika Steelworks in Menderes.
Can you stress-relieve before machining?
Yes, when the drawing or the tolerance needs it, large weldments are stress-relieved before finish machining.
How do large parts get to Europe?
On purpose-built cradles, by road or container from İzmir. We agree the Incoterm, lifting points and packing on the quotation.
Which documents do you supply?
EN 10204 3.1 certificates with every order, dimensional reports, and 3.2 certificates or third-party inspection on request.
Heavy Machining in Türkiye for European Machine Builders
Large parts are where many supply chains get stuck. Few suppliers can turn a three-metre flange, mill a four-metre machine bed or bore a heavy gear housing, and those that can are often fully booked. Our family group runs a dedicated 1,600 m² machining plant in Kemalpaşa, İzmir, for exactly this work, and Nika Steelworks manages every order placed there.
Vertical turning to Ø4,200 mm
Rings, flanges, drums, hubs and slewing-ring seats are turned on vertical lathes, the largest a Dalian YiMei CKQ5240 with a Ø3,160 mm chuck, Ø4,200 mm swing and 2,500 mm height. Faces stay flat and diameters concentric because the part lies on the table instead of hanging in a chuck.
Boring and milling up to 4,500 mm
Machine beds, frames and housings are machined on Doosan DBC 130L, Scharmann and WFL boring mills, with tables up to 2,000 × 1,500 mm and 40-tool changers. Bores, faces and bolt circles are machined in as few set-ups as possible to hold their position to each other.
Machined weldments from one supplier
Most large parts are welded first. We weld to EN 1090 EXC3 and ISO 3834-2, plan machining stock at fit-up and machine after welding, so the datum used in fabrication is the datum used in machining. Parts are then painted, cradled and shipped.
Handling and delivery
Overhead cranes lift up to 12 tonnes. Heavy parts leave on purpose-built cradles for road or container transport to Europe. See the machine park, our rotary mandrel project, or send your drawing. For smaller and serial parts, see CNC machining.
Send a drawing for a large part.
Include material, weight, critical tolerances and coating. We confirm the machine, handling and lead time in writing.